Measured shape, fitted surfaces.
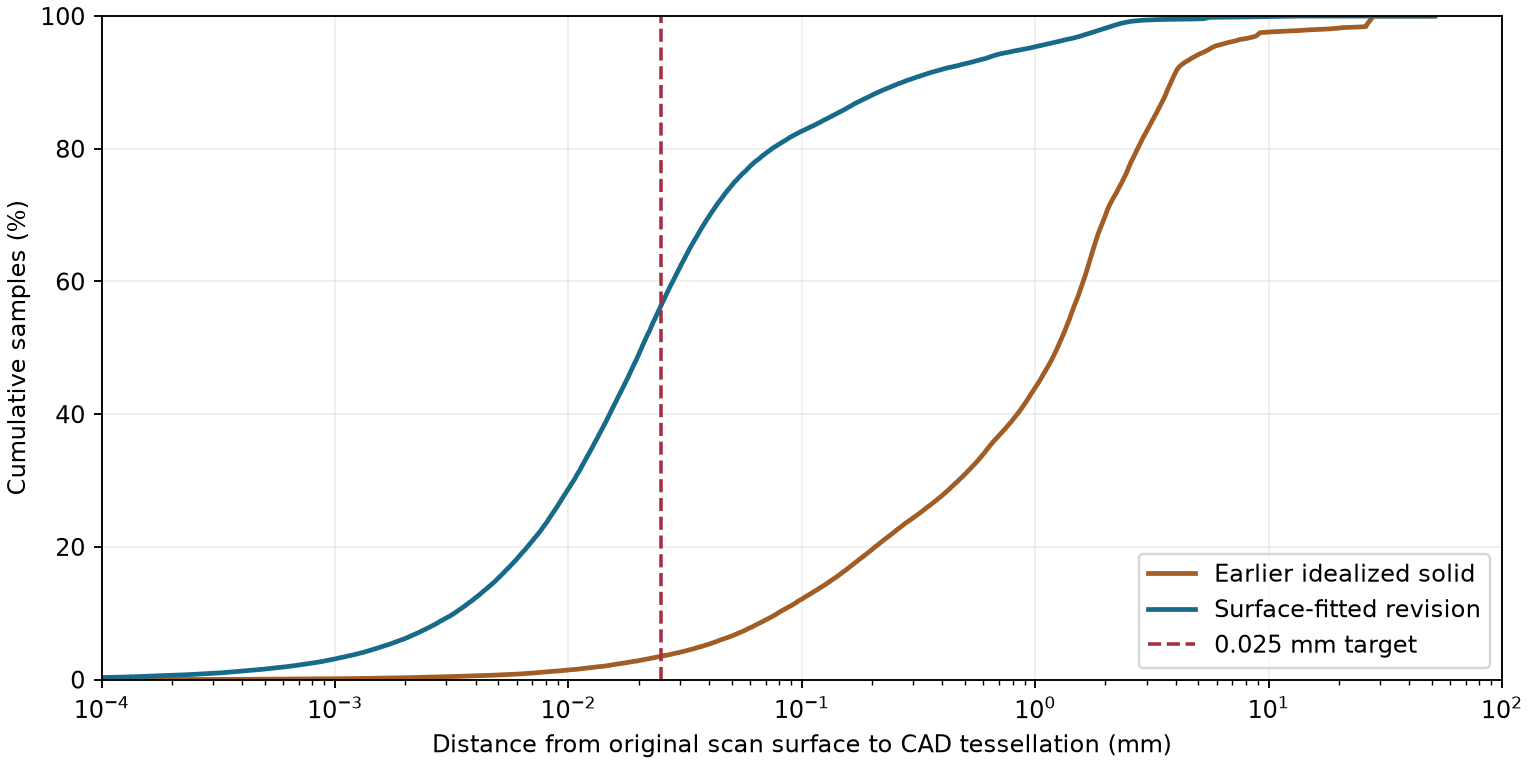
Tolerance comparison.
A smooth B-spline CAD reconstruction of the shaft and two spiral flights, compared with the earlier constant-pitch idealization using the same held-out source samples.
Open interactive model · Download new STEP assembly · Raw comparison CSV · Full JSON report
56.5% of the primary holdout sample lies within 0.025 mm. This compares geometry with the supplied STL; it does not certify scanner accuracy or manufacturing tolerances.
Primary comparison: equal source surface area
80,000 random points on original STL triangles, weighted by triangle area. Training facets are excluded. Both revisions use the same alignment and the same test points. Values are unsigned nearest-surface distances.
| Metric | Earlier solid | Surface-fitted |
|---|---|---|
| Mean | 2.0802 mm | 0.1661 mm |
| Median | 1.2450 mm | 0.0206 mm |
| RMS | 4.3468 mm | 0.6766 mm |
| 95th percentile | 5.5715 mm | 0.8926 mm |
| 99th percentile | 26.7554 mm | 2.4026 mm |
| Maximum sampled | 51.7637 mm | 51.1658 mm |
| Within 0.025 mm | 3.5112 % | 56.4712 % |
| Within 0.100 mm | 12.1225 % | 82.6713 % |
| Within 0.250 mm | 22.2988 % | 89.5775 % |
| Within 0.500 mm | 30.9675 % | 92.8175 % |
Where the differences remain
Automatic region labels are based on radius, surface normal and helical phase. Root boundaries are approximate. Distance columns are in millimeters; all regions, including difficult ends, are retained in the overall comparison.
| Source region | Samples | Old median | New median | New P95 | New max | Within 0.025 |
|---|---|---|---|---|---|---|
| bore observed | 2,652 | 22.7993 | 0.0197 | 0.1897 | 3.7159 | 57.9% |
| ends roots other | 5,414 | 1.5600 | 0.9477 | 5.3367 | 51.1658 | 0.3% |
| flight tips | 3,168 | 0.8109 | 0.0156 | 0.1355 | 2.2650 | 69.0% |
| shaft outer | 35,304 | 0.4491 | 0.0183 | 0.2562 | 3.9311 | 62.9% |
| spiral a faces | 16,881 | 2.2354 | 0.0191 | 0.2361 | 2.0027 | 58.3% |
| spiral b faces | 16,581 | 1.9148 | 0.0199 | 0.2931 | 17.1237 | 56.7% |
Largest retained discrepancies
The largest deviations include source geometry outside the fitted auger envelope. It has not been established to be scanner noise. These points remain in all overall statistics; difficult geometry has not been discarded to improve the reported result.
| Source facet index | Region | Earlier (mm) | Fitted (mm) |
|---|---|---|---|
| 18965038 | ends roots other | 51.7637 | 51.1658 |
| 18844867 | spiral b faces | 18.7202 | 17.1237 |
| 18042140 | ends roots other | 12.7299 | 13.5883 |
| 17641701 | ends roots other | 14.1236 | 13.5705 |
| 17884274 | ends roots other | 12.2138 | 13.5314 |
| 17680290 | ends roots other | 13.8571 | 13.5220 |
| 17828924 | ends roots other | 12.8345 | 13.5121 |
| 17854017 | ends roots other | 13.8901 | 13.4840 |
| 17946539 | ends roots other | 12.8484 | 13.4446 |
| 17686880 | ends roots other | 14.3876 | 13.3870 |
| 18844789 | spiral b faces | 15.4481 | 13.2852 |
| 17811592 | ends roots other | 14.4379 | 13.2797 |
Sensitivity to scan sampling density
A second 80,000-point holdout gives each source triangle equal probability. This emphasizes densely tessellated regions instead of equal physical surface area. It must not be substituted selectively for the primary result.
| Metric | Earlier solid | Surface-fitted |
|---|---|---|
| Mean | 1.9775 mm | 0.1678 mm |
| Median | 1.1794 mm | 0.0200 mm |
| RMS | 4.1691 mm | 0.6777 mm |
| 95th percentile | 5.1384 mm | 0.9407 mm |
| 99th percentile | 26.5698 mm | 2.3948 mm |
| Maximum sampled | 51.1256 mm | 50.5367 mm |
| Within 0.025 mm | 3.7125 % | 57.2600 % |
| Within 0.100 mm | 12.7525 % | 82.8175 % |
| Within 0.250 mm | 23.0700 % | 89.4363 % |
| Within 0.500 mm | 31.8613 % | 92.6250 % |
Reverse check: CAD to the full source mesh
20,000 area-uniform samples on each fine CAD tessellation, nearest distance against ALL 19,022,751 original source triangles in streamed blocks. Inferred central bore subset is approximate by location; other closure/root assumptions remain. Distance columns are in millimeters. Large reverse distances can identify added surfaces or missing scan coverage; they do not establish whether an inferred internal surface is physically correct.
| CAD samples | Median | P95 | Maximum sampled |
|---|---|---|---|
| Earlier: all surfaces | 1.2319 | 4.7133 | 39.7027 |
| Fitted: all surfaces | 0.0549 | 9.4991 | 20.5135 |
| Fitted: excluding approximate inferred central bore region | 0.0265 | 7.3717 | 20.5135 |
4,612 of the 20,000 new-CAD samples were tagged as belonging to the approximately inferred central bore region.
CAD validation
| Part | Faces | Volume (mm³) | Validation |
|---|---|---|---|
| shaft | 15 | 5,214,116.8 | Valid, closed; STEP re-import passed |
| spiral-a | 6 | 979,863.8 | Valid, closed; STEP re-import passed |
| spiral-b | 6 | 1,010,818.9 | Valid, closed; STEP re-import passed |
These are smooth CAD boundary-representation solids. Volumes depend on the inferred interior and are not measured volume certificates. Separate parts may overlap slightly at construction interfaces.
How noise was reduced
The helix estimate provides a coordinate system, not the final shape. Each side of each flight is fitted independently using robust cubic B-splines, with 5 mm axial and 6 mm radial knot spacing. Large residuals are downweighted using a 0.07 mm robust scale. The shaft uses locally weighted Fourier profiles that allow bending and ovality: an 18 mm neighborhood, 4.5 mm Gaussian weighting scale and five harmonics. These smoothing parameters are not accuracy guarantees.
Fitting uses every 23rd original facet centroid. All such facets are excluded from holdout evaluation. Neighboring scan facets remain spatially correlated, so this is a geometric holdout, not an independent measurement campaign.
Assumptions requiring review
- Central bore is inferred between sparse observed inner surfaces; hidden depth and transitions are not verified.
- Bore step transitions use estimated axial positions; end caps are regularized.
- Flight roots extend 0.08 mm into the fitted shaft for construction; welds and the true concealed interfaces are not reconstructed.
- The three solids are an assembly; small construction overlaps can remain at roots.
- Smoothness settings are not a guarantee of measurement accuracy.
Numerical and measurement limits
Requested absolute CAD tessellation deflection: 0.0025 mm; angular tolerance: 0.05 rad. Earlier mesh: 1,522,416 triangles; new mesh: 9,128,616 triangles. Distances are computed against these fine meshes, not exact analytic projection. Requested meshing deflection is not an independently certified error bound. Browser display meshes are reduced further and must not be used to assess the 0.025 mm target.
- This is a geometric comparison with the supplied scan, not a scanner calibration or manufacturing certificate.
- Sampled maximum is not a full-surface Hausdorff bound.
- Hidden central bore and step closures are inferred and cannot be tolerance-verified from missing scan data.
- Spiral roots/welds and local damaged or repaired regions need further review.
- Fit settings regularize local surfaces; they cannot prove which small features are scan noise versus real defects.
- The largest deviations include source geometry outside the fitted auger envelope. These samples are retained; the geometry has not been established to be scanner noise.
Provenance
Source: SM_260_FA_0.06328_Mesh_fill_1.stl · 19,022,751 original triangles. Units: user-selected millimeters. The source file was preserved.
SHA-256: 54ba9203cc540e31163d2742e2f6e3bdc8b499212304fd84259ba67b9f3a1ff1